A drawing says one thing. The purchase order says another. The mill ships what the PO said, and your yard stops. Here is how to keep all three documents saying the same thing.
Preventing errors when ordering marine angle steel by drawing comes down to four habits: read the callout exactly as the designer wrote it, name the dimensional standard and its edition on the purchase order, tie every order line to a specific drawing revision, and confirm the final specification block with the supplier in writing before production starts.
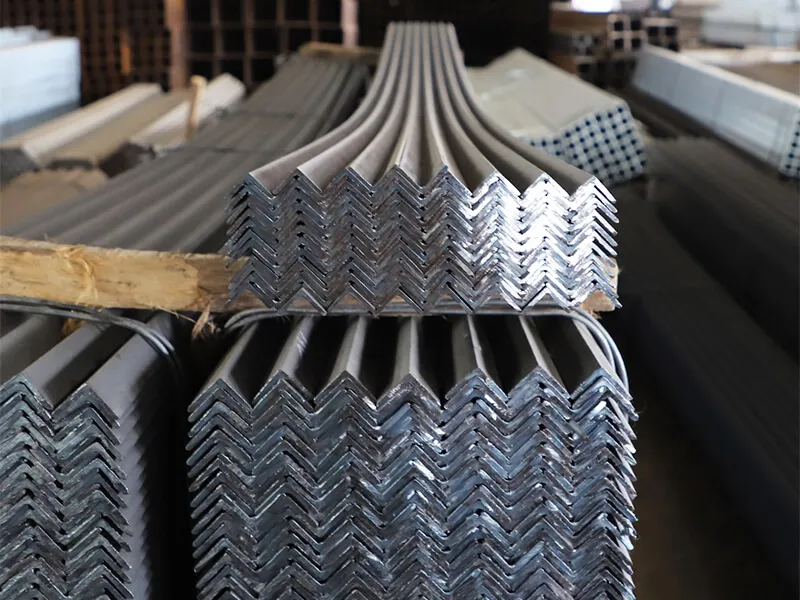
I have handled marine angle steel orders out of Liaocheng for years, and the pattern never changes. The steel is almost never the problem. The gap between the drawing and the order text is the problem. A mill reads your purchase order. It does not read your drawings, because in most cases we never receive them. So every number the drawing holds must travel onto the order, word for word, or the mill fills the blank with its own assumption. Sometimes the assumption is right. When it is wrong, the cost is not the steel — it is the three weeks your frames sit on the quay while a replacement order rolls. This article walks through the three places those gaps open up, and the exact habits that close them.
How Should You Read a Marine Angle Steel Callout on a Shipbuilding Drawing?
Most ordering errors start in the first five seconds, at the callout itself. A wrong reading of three numbers turns into a full order of the wrong section, and nobody notices until fit-up day.
Read a marine angle callout as three values: first leg length, second leg length, then thickness, all in millimetres. For equal angles both legs are the same; for unequal angles, the first number is the longer leg. The callout never shows the root radius, the toe radius, or the grade — those must be stated separately.
That sounds simple, and every buyer I know would agree they know it. Yet the single most expensive order error I have personally witnessed came from a callout, not from a mill mistake. Let me walk through the way a callout actually behaves on a real drawing, because the details are where the traps sit.
What the Three Numbers Do and Do Not Tell You
A callout such as L150x90x12 tells you the long leg is 150 mm, the short leg is 90 mm, and the nominal thickness of both legs is 12 mm. That is all it tells you. It does not tell you the root radius r1, the inner curve where the two legs meet. It does not tell you the toe radius r2, the small rounding at the tips. It does not tell you the grade, the society, the impact test temperature, or the length. It also does not tell you which leg the designer considers critical. That last one matters more than buyers expect.
On a hull frame, sometimes the long leg carries the load into the shell plating. Sometimes the short leg is the one that must match a prefabricated bracket slot. The callout gives you both leg lengths, so the geometry is complete — but only if you copy both numbers onto the order. If you write “12 mm AH36 angle” and drop the section, the mill has to guess which leg the 12 mm belongs to. In the version of this story I saw play out with a yard in Vietnam, the purchase order said “12mm AH36 angle” and the drawing needed the short leg at 12 mm. The mill rolled the long leg at 12 mm and the short leg at 10 mm — a standard section in its own table. Every document was correct. The steel was scrap for that project, and the reorder plus idle labor ran into six figures.
The Callout Variations That Catch Buyers
Drawings do not always use the same notation. JIS-influenced yards may write the callout with the profile name first. European yards following EN 10056 may give the section as a designation like L 150 x 90 x 12 with the root radius stated separately. Some material lists abbreviate entirely and write “L150x90x12” with no grade at all, because the grade lives in a separate column. None of this is wrong, but each format shifts information somewhere else, and the person building the purchase order has to collect all of it.
The table below shows how to translate the common callout forms into a complete order line. Use it as a checklist when you transcribe from drawing to PO.
| Drawing callout | How to read it | What is missing from the callout |
|---|---|---|
| L 150x150x12 | Equal angle, both legs 150 mm, thickness 12 mm | Grade, society, standard, length, radius |
| L 150x90x12 | Unequal angle, long leg 150 mm, short leg 90 mm, thickness 12 mm | Same as above, plus which leg is design-critical |
| L200x90x8x14 | L-profile where 8 and 14 are the two leg thicknesses | This is an L-shaped section, not a plain angle — different rolling programme |
| HP200x9 | Bulb flat, web 200 mm, flange thickness 9 mm | Not an angle at all — do not let a summary list merge the two families |
| “Angle 12 mm AH36” (verbal or shorthand) | Incomplete | Section dimensions entirely — never let this reach a PO |
That fourth and fifth row deserve a moment. Mixed families are a quiet source of errors, because a ship hull uses angles, bulb flats, and L-sections side by side, and a summarized material list can blur them. I always ask buyers to send the material list in its original column structure rather than a pasted summary. It takes them one minute. It saves us both a clarification round that used to take three days.
My Port-Side Rule About Callouts
Here is the habit I picked up from watching receiving crews check containers at Dammam: the fastest handover I ever saw was for a buyer whose purchase order repeated the callout in full on every single line, section included, even when it was repeated twenty times. Redundant, yes. But the receiver never had to open a drawing at the quay. He checked the stamp against the order line and signed. The slowest handovers were always the orders that said “as per drawing” — because nobody at the port had the drawing. Redundancy on paper is cheap. Redundancy at the quay is expensive. Write the full callout every time.
Which Tolerances and Standards Must the Order Name to Match the Drawing?
A callout copied correctly is still not a complete order. Two mills can both roll “L150x90x12” and deliver sections that behave differently in your assembly, because they rolled to different tolerance standards.
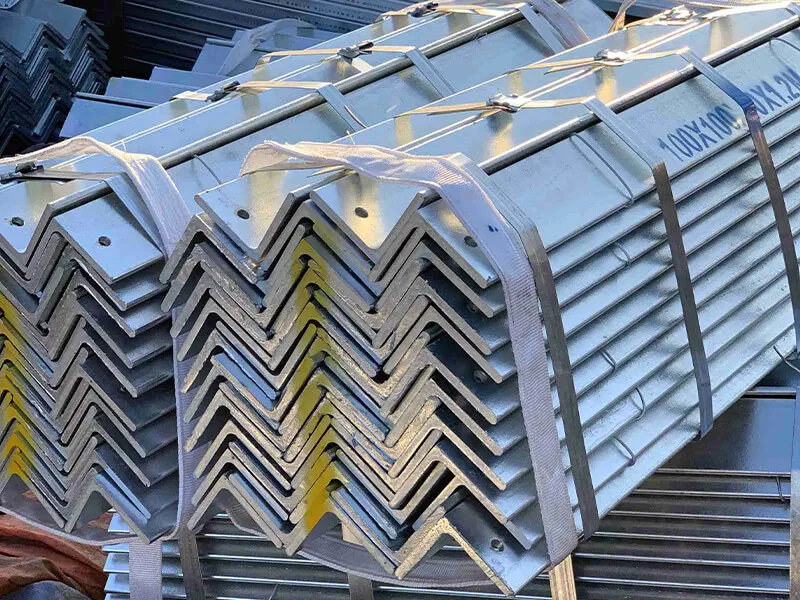
The order must name the governing dimensional standard and its edition — JIS G3192, EN 10056, or the class society rule — because the standard fixes the acceptable variation in leg length, thickness, straightness, and twist. Without it, the mill applies its own default, and the steel may not fit the drawing even though every nominal dimension is correct.
Why the Standard Matters More Than the Nominal Size
The nominal size is what the designer cares about. The tolerance is what the fitter cares about. A 150 mm leg delivered at 148 mm is inside several mills’ default tolerance, and the certificate will honestly report a conforming product. But if the drawing was detailed around a true 150 mm, that 2 mm gap shows up at every bracket, and the crew grinds or shims their way through days of rework that no purchase order budgeted for. I have seen exactly this with a 150x90x9 shipment: the certificate was clean, the yard still had to rework every bracket, and the argument afterwards was unwinnable because the order never named a tolerance standard. Both sides were right, and the yard still lost three days.
When you name the standard, the mill pins its rolling and its inspection to a written envelope. When you do not, the mill pins it to habit. Our own quotation practice reflects this: when a customer names the standard, we state the tolerance line back to them explicitly and the mill test certificate reports actual measured values. When they do not, we still ship to a standard — but we pick it ourselves. Most of the time we guess right. “Most of the time” is not a procurement strategy.
The Numbers Behind JIS G3192
Because so many shipbuilding angle orders run to JIS G3192, it is worth knowing what that standard actually allows. The table below collects the side-length and thickness tolerances buyers ask me about most.
| Dimension | Range | JIS G3192 tolerance |
|---|---|---|
| Side length A or B | below 50 mm | ±1.5 mm |
| Side length A or B | 50 to under 100 mm | ±2.0 mm |
| Side length A or B | 100 to under 200 mm | ±3.0 mm |
| Side length A or B | 200 mm and over | ±4.0 mm |
| Thickness, A under 130 mm | t under 6.3 mm | ±0.6 mm |
| Thickness, A under 130 mm | t 6.3 to under 10 mm | ±0.7 mm |
| Thickness, A under 130 mm | t 10 to under 16 mm | ±0.8 mm |
| Thickness, A 130 mm and over | t 6.3 to under 10 mm | ±0.8 mm |
| Thickness, A 130 mm and over | t 10 to under 16 mm | ±1.0 mm |
| Thickness, A 130 mm and over | t 16 to under 25 mm | ±1.2 mm |
Three observations from this table, drawn from years of reading certificates against drawings. First, the side-length windows are generous — a 150 mm leg can legally arrive at 147 mm under this standard. If your design needs tighter, say so on the order; mills can select or straighten, but only if they know. Second, thickness tolerances are asymmetric in practice at some mills, and the minimum thickness is what governs strength — measure at the middle of the leg, not the corner, when you verify on receipt. Third, straightness and twist live outside this table in most discussions, yet they cause more fit-up pain than length or thickness. Under JIS practice a bow of roughly 1 mm per metre is a common acceptance line, and a twist that lets one corner lift more than about 1 mm per metre will get a batch rejected at a strict yard. If your project cares, put the straightness and twist limits on the order in writing.
Drawing Revision Control — the Silent Half of Tolerance
There is a second dimension to “matching the drawing” that has nothing to do with steel: which revision of the drawing are you ordering from? Ship drawings get revised. A frame spacing changes, a bracket thickens, a section moves from 10 mm to 12 mm. If the purchase order references “the drawing” with no revision number, and the mill’s production copy is two revisions behind yours, both parties execute faithfully and the result is still wrong. I ask every buyer to put the drawing number and revision letter on each order line: “L150x90x12, dwg 5312-B rev 3”. When a revision lands mid-order, the buyer sends a written amendment with the new rev, and the mill confirms in writing which rev it is rolling to. It is a one-line habit, and it kills an entire family of disputes before they exist.
What Does a Drawing-Proof Purchase Order Line Actually Look Like?
The last step is assembling everything above into the order text itself. This is where good intentions become a document a mill clerk can execute without guessing.
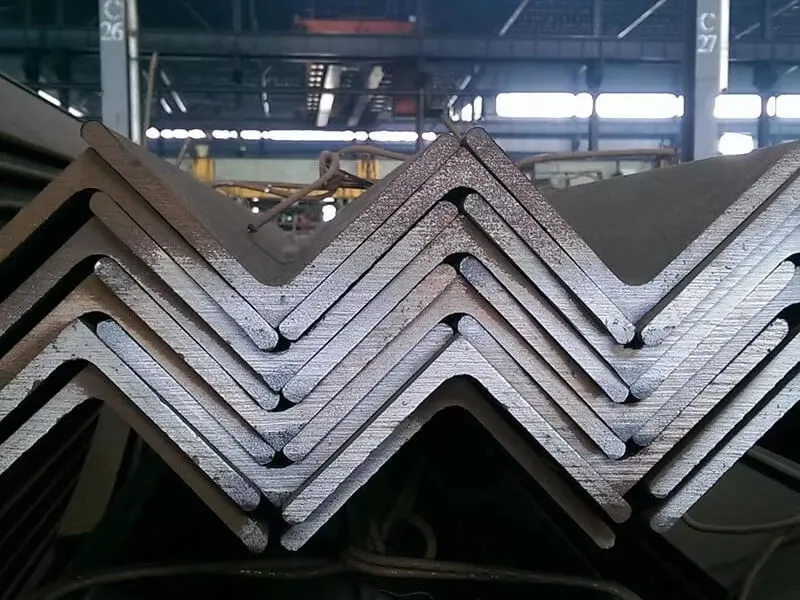
A drawing-proof order line states the full section, both leg lengths and thickness, the dimensional standard with edition, the grade with society prefix, the impact test temperature, the delivery condition, the length and its tolerance, the certificate class, the marking requirement, and the quantity in pieces and tonnes — each on its own line, tied to a drawing revision.
I recommend buyers build this once as a template and reuse it, because the errors cluster around orders written under time pressure. Here is the block my team fills in with customers, line by line. Feel free to copy it directly into your own PO template.
| Order line | What to write | Example entry |
|---|---|---|
| Section | Full callout, both legs | L150 x 90 x 12 |
| Dimensional standard | Name plus edition | JIS G3192 |
| Grade and society | Prefix included | ABS AH36 |
| Impact test | Temperature and direction | Charpy V-Notch at 0 °C, longitudinal |
| Delivery condition | Rolling route | As-rolled (state normalized if required) |
| Length | Type, value, tolerance | Exact 9,000 mm, +10 / −0 mm |
| Certificate | EN 10204 class | 3.1 (3.2 when the surveyor requires it) |
| Marking | What is stamped or tagged | Heat number, grade, size on every piece |
| Drawing reference | Number and revision | dwg 5312-B rev 3 |
| Quantity | Pieces and theoretical weight | 180 pieces, about 26.5 tonnes |
Two of these lines do more work than they look like they do. The impact test line exists because an AH36 is only an AH36 for your project if the Charpy test ran at the temperature your design assumes; a certificate without a stated test temperature does not close that loop. The marking line is what lets a two-person receiving team clear a container in an hour instead of a day, because every bundle carries its own identity and nobody sorts steel by looking at it.
The Comparison Buyers Should Run Before Signing
Before the order goes out, run one last comparison — not of prices, but of documents.
Put the drawing callout, the material list entry, and the purchase order line side by side and confirm they agree on every value. The table below is the checklist I use myself when a customer asks me to sanity-check their PO against their drawing before production.
| Error source | How it shows up | Prevention on the order |
|---|---|---|
| Callout misread (leg vs thickness) | Wrong section arrives; certificate is technically correct | Write A x B x t in full; never shorthand to one dimension |
| No dimensional standard named | Steel does not fit brackets despite correct nominal size | Name JIS G3192 / EN 10056 with edition year |
| Wrong drawing revision | Order matches an outdated frame schedule | Quote drawing number and revision on every line |
| Missing society prefix | Certificate grade does not satisfy classification | State “ABS AH36”, not just “AH36” |
| Ambiguous length | Mill ships random lengths; cutting plan collapses | State exact length with plus/minus tolerance |
| Family mix-up (angle vs bulb flat vs L-section) | Summary list blurs product families | Send the material list in original columns |
| Verbal specification | Nothing to check at receiving; disputes unwind | Everything in writing on the PO, no phone-only changes |
One thing I would add from the supplier side, because buyers rarely hear it: we would rather answer three written questions before production than one complaint after delivery. When Gulf Metal Solutions in Saudi Arabia started sending their enquiries with the full specification block attached, the clarification rounds between us dropped to almost nothing, and their SGS pre-shipment inspections started closing on the first pass. Their team told us the packaging and paperwork were the cleanest they had received from any plate supplier. That is what a complete order line buys — not just correct steel, but a supply chain that moves without friction. If you want a second pair of eyes on a drawing-to-PO transcription, send both to me at sale@sdyichen.cn and I will check the callouts against our rolling tables before you commit.
Conclusion
Read the callout in full, name the standard, pin the revision, and put every value on the order line. Thirty seconds of transcription discipline protects weeks of fabrication schedule.