A takeoff sheet with one broken column costs a yard a second order, a second freight bill, and a month of schedule. The fix is structural, not arithmetic.
A reliable marine angle steel takeoff sheet is a revision-controlled table with one row per line item. Each row carries block, drawing revision, profile, grade, cut length, position count, kg/m, weight, and a heat reference. Three checks then reconcile pieces, weight, and bar count before purchasing.
Most of the takeoff sheets I receive are not wrong because the estimator cannot multiply. They are wrong because the sheet has no structure to stop a small error from travelling. A number gets typed once, copied four times, and by the time it reaches purchasing nobody can say which drawing it came from. I have watched a 22-tonne order go out on a sheet that mixed two grades into one line. The steel was perfect. The paperwork was not, and the yard paid for the mistake twice.
So this is not an article about formulas. It is about the sheet as a document. Build the document properly and the arithmetic has somewhere to fail safely.
What Columns Must a Marine Angle Steel Takeoff Sheet Carry?
A sheet missing the grade string or the block code still adds up. It just cannot be ordered, inspected, or defended.
Carry ten columns: item number, block, profile, grade string, cut length, positions, total pieces, kg/m, total weight, and heat or MTC reference. Every row must point to one drawing and one approved revision. If a column cannot be filled at takeoff stage, leave it blank rather than guessing.
Nine Columns, One Row per Member
The table below is the version I send to new buyers. It is deliberately narrow. Every column exists because I have seen an order fail without it.
| Column | What goes in it | What breaks without it |
|---|---|---|
| Item no. | A fixed number that never changes when rows are inserted | Rows get renumbered and the purchasing list stops matching the nesting file |
| Block | Hull block or zone code from the block division drawing | Steel arrives as one pile and the fitting crew sorts it on the ground |
| Profile | Leg × leg × thickness, equal or unequal leg | The saw picks the nearest bar on the rack instead of the right one |
| Grade string | Society, grade, delivery condition, certificate type | The surveyor cannot match the MTC to the approved drawing |
| Cut length | Net finished length in millimetres | The saw adds or drops a trim allowance by habit |
| Positions | Number of identical places shown on the drawing | Pieces get counted by eye and the error multiplies |
| Total pieces | Positions × sides × tiers | Port and starboard drift apart without anyone noticing |
| kg/m | Table value for that exact profile | Weight is rebuilt from a formula that always runs light |
| Total weight | Pieces × cut length × kg/m | Purchasing rounds the tonnage instead of the bar count |
| Heat / MTC ref | Heat number once steel is allocated | Traceability dies at the first cut |
Ten columns, one row per member. That is the whole design. A row is not a summary of a group of parts. It is one member, at one size, in one grade, in one block.
The Grade String Is Not a Nickname
“AH36” is not an orderable line. AH36 under ABS, AH36 under LR, and AH36 under CCS come from different approval routes, different certificate sets, and often different mills. Your surveyor will care which one arrived.
I ask buyers to copy the grade string character for character from the approved drawings, society first. If the drawing says equal angle, grade B, LR, then the sheet should not say A grade, any society. A yard in Romania [Zora will replace] learned this when a surveyor refused a bulkhead stiffener set because the MTC carried an endorsement the approved drawing did not list. The bars were fine. They sat in the store for weeks while a re-inspection cleared them.
This costs nothing to prevent. Open the plan approval document once, copy the string once, and every quotation, certificate, and inspection conversation downstream lines up automatically.
Last month I stood in our yard in Liaocheng while a bundle was opened for a buyer’s inspector. The bars were bundled by size, and every bundle carried a paper tag with the heat number written in marker. The inspector checked three tags against the MTC. Two matched. The third had faded until only four digits were readable, and he put the bundle on hold. Nothing was wrong with the steel. The tag was. That is why the heat column on my sheets gets filled at allocation, not at delivery, and why I ask buyers to keep the tag with the bar after cutting. For the longer version of that handoff, see how to match marine angle steel orders with shipbuilding material lists.
Why Cut Length Belongs on the Sheet and Bar Length Does Not
The takeoff sheet records what the ship needs. It does not record what you buy. Cut length is net, in millimetres, with no trim and no kerf. Bar length is a purchasing decision made later, after nesting.
When estimators put 12 m bars into the takeoff, two things go wrong. The weight stops matching the drawing, because bars include offcut. And the sheet stops being reusable, because every new stock length forces a rewrite. Keep the sheet clean and let the nesting file carry the bar count.
How Do You Keep the Sheet Tied to the Drawings It Came From?
A takeoff is only as good as the revision it was built from. Most quantity disputes are revision disputes wearing a costume.
Tie every sheet to one drawing revision. Put the drawing number, revision letter, and issue status in the header. Freeze the file when it is issued for construction, and log every change with its weight effect and the person who approved it.
Header Before Rows
The header is where a sheet earns trust. It needs five things: project and hull number, drawing number and revision letter, issue status, preparer, and date. Add a sixth field for the class society if the project has more than one.
Issue status matters more than people expect. A sheet marked “for quotation” and a sheet marked “for construction” look identical once they are printed. One is allowed to be five percent rough. The other is a commitment. I have seen a quotation sheet get forwarded to a mill because nobody checked the status line, and the mill rolled to a number that was never approved.
Revision Letters Beat Dates
Dates are ambiguous across time zones and email threads. Revision letters are not. When a drawing goes from C to D, the sheet goes from C to D on the same day, and the old file gets archived, not overwritten.
My rule is simple. One sheet per drawing revision. If a revision changes only one block, you still issue a new sheet revision, because the purchasing file must be able to answer the question “which drawing was this bar cut to” two years later.
The Change Log Is the Real Deliverable
The change log is the part everyone skips and the part that saves the most money.
| Revision event | What moves in the sheet | Who must sign |
|---|---|---|
| Bracket or clip detail added | Piece count and total weight | Design office and yard planning |
| Frame spacing changed | Position count on every frame line | Design office |
| Grade upgraded in one block | Grade string and certificate scope, weight unchanged | Design office, class, and owner |
| Profile swapped for an equivalent | kg/m and bar count | Design office and class |
| Block boundary moved | Block allocation, not total weight | Yard planning |
| Nesting shows a bar break | Purchase quantity only | Planning and procurement |
Read the fourth row again. A grade upgrade can leave the weight identical and still change the price by a wide margin and the certificate package completely. A sheet that only tracks tonnage will report “no change” and mean it. That is how a yard ends up with AH36 steel certified to the wrong society and no paper trail to show when it happened.
Freeze It, Then Version It
Use one master file with protected formula cells. Export a locked PDF at every issue. Never accept a file called final_final_v3 from an email thread as the working copy, because two people will edit two copies and the difference will surface at the saw.
Which Checks Prove the Takeoff Sheet Is Right Before You Order?
Adding a column of numbers proves nothing. The sheet is right when three independent methods land on the same quantity.
Run four checks: count positions in both directions, rebuild the weight from table kg/m, convert the weight into bars, and compare the total with the design office estimate. If any check misses by more than its band, stop and find the row that caused it.
Check One: Count Positions in Both Directions
Take one frame line. Count the positions from the drawing, then count them again from frame spacing. They must agree.
A 24 m block at 600 mm spacing gives 40 spaces. But 40 spaces need 41 frames, because both ends carry one. Estimators who divide and stop at 40 are one frame short per line, and that error repeats on every line in the block. Then multiply by two sides, and the shortfall doubles.
Write the arithmetic into the sheet as a note, not in your head. The note is what lets the next person check your work without re-reading the drawing.
Check Two: Rebuild the Weight from kg/m
The formula is [(A + B) − t] × t × 0.00785, where A and B are leg lengths in millimetres and t is thickness. It is correct, and it is always light, because it ignores the root radius that hot rolling leaves in the corner.
| Profile | Formula kg/m | Table kg/m | Gap |
|---|---|---|---|
| L75 × 75 × 6 | 6.78 | 6.85 | +1.0% |
| L100 × 100 × 10 | 14.92 | 15.10 | +1.2% |
| L125 × 125 × 10 | 18.84 | 19.10 | +1.4% |
| L150 × 90 × 12 | 21.48 | 21.50 | +0.1% |
| L150 × 150 × 12 | 27.13 | 27.30 | +0.6% |
| L200 × 200 × 16 | 48.23 | 48.50 | +0.6% |
Use the formula to check the table, not to replace it. If your sheet weight sits one to one and a half percent below the table weight for the same metres, the sheet is probably right and the formula is doing its usual job. If it sits five percent below, a row is missing.
Check Three: Turn the Weight into Bars
This is the check that catches scope errors no weight comparison can find.
Take 480 m of L100 × 100 × 10. At 15.1 kg/m that is 7,248 kg. In 12 m bars it is 40 bars, before kerf and end trim. Now look at the purchase quantity on the sheet. If purchasing wrote 7.2 tonnes and 38 bars, the weight and the bar count disagree, and one of them is lying.
Do this for every profile on the sheet. The bar count is the number the saw actually consumes, so it is the number most likely to expose a bad cut length. Remember the ±50 mm length tolerance on mill bars and keep at least 100 mm of slack per bar in the nest. A bar that arrives at 11.95 m will break a nest planned to 12.00 m exactly.
On the quay, the bar count is also what the stevedore counts, not the tonnage. I have stood at the rail of a loaded barge while a tally clerk marked bundles against a sheet that carried tonnes only. The count took twice as long, because nobody had written the piece number down. One extra column saves that hour. It also gives the receiving team a number they can check without opening a single bundle.
Check Four: Compare with the Estimate You Already Had
Design offices publish structural weight estimates at each stage. The published allowance bands are useful: a weight calculated from a material takeoff at concept stage carries roughly a 10 percent allowance, and one calculated from approved-for-construction drawings carries roughly 5 percent.
If your finished sheet is 15 percent above the approved-for-construction estimate, one of the two documents is wrong. Do not average them. Find the block that grew and read its revision history.
| Check | What it proves | What it catches | Accept band |
|---|---|---|---|
| Position count both ways | The drawing was read, not estimated | Off-by-one at bulkheads | Exact match |
| Weight rebuilt from kg/m | Arithmetic and profile selection are clean | Wrong kg/m, unit slip | Within 1% |
| Weight turned into bars | The order can actually be nested | Tonnage rounded instead of bars | One bar per profile |
| Compare with design estimate | The sheet covers the right scope | Missing block or missing detail | Within 5% of approved estimate |
Which Mistakes Most Often Break a Marine Angle Steel Takeoff Sheet?
The expensive errors are boring. They are the same six mistakes, repeated on every second sheet I receive.
The most common failures are double counting port and starboard, counting frames instead of positions, leaving out brackets and clips, merging grades to shrink the total, and mixing millimetres with metres. Each one is cheap to prevent and expensive to discover at the saw.
Double Counting Port and Starboard
Symmetry feels like a shortcut. Copy the port column, paste it into starboard, and the total doubles. But not every member is mirrored. Pipe supports, ladder brackets, and machinery seat details often exist on one side only. The mirrored copy adds steel that will never be welded.
The fix is a column, not a warning. Add “sides” as its own field with values 1 or 2, so the multiplier is visible and reviewable. When a row says 2, someone can ask why.
Counting Frames Instead of Positions
Frames and positions are not the same word. A frame is a member. A position is a place where a member goes. On a curved shell, one frame position can take two or three separate angle pieces with different cut lengths.
If the sheet has one row per frame but the drawing shows three pieces at each frame, the sheet is short by two thirds on that line, and the weight check will not catch it because the kg/m is right.
Forgetting the Small Stuff
Brackets, clips, lugs, floors, bulkhead stiffeners, ladder stringers, and platform edges are all angle steel. Together they often add 10 to 15 percent to a frame count. They are also the first things skipped when a sheet is built quickly from the main structural plan.
I keep a fixed “small parts” section at the bottom of every sheet, one row per detail type, with a note on which drawing it came from. If the section is empty on a real vessel, the sheet is incomplete, not efficient. The same logic sits behind how to estimate cutting losses when purchasing marine angle steel: the parts you forget are the parts you reorder at spot price, with a second freight bill attached.
Merging Grades to Shrink the Total
A single tonnage figure is easier to quote. It is also impossible to order correctly. Grade A and AH36 are different lines, different certificates, and different prices. Merging them hides the split from purchasing and from the surveyor.
Sort the sheet by grade first, then by profile. The total will be the same. The order will be buildable.
Millimetres in a Metre Column
This one is embarrassing and common. A cut length of 4,800 gets typed into a column headed “m” and becomes 4.8, or the reverse. The row still looks plausible.
Lock the units into the header text, not into a comment. Write “Cut length (mm)” and “Total weight (kg)”. Then add one summary cell that divides total weight by 1,000 so purchasing reads tonnes without retyping anything.
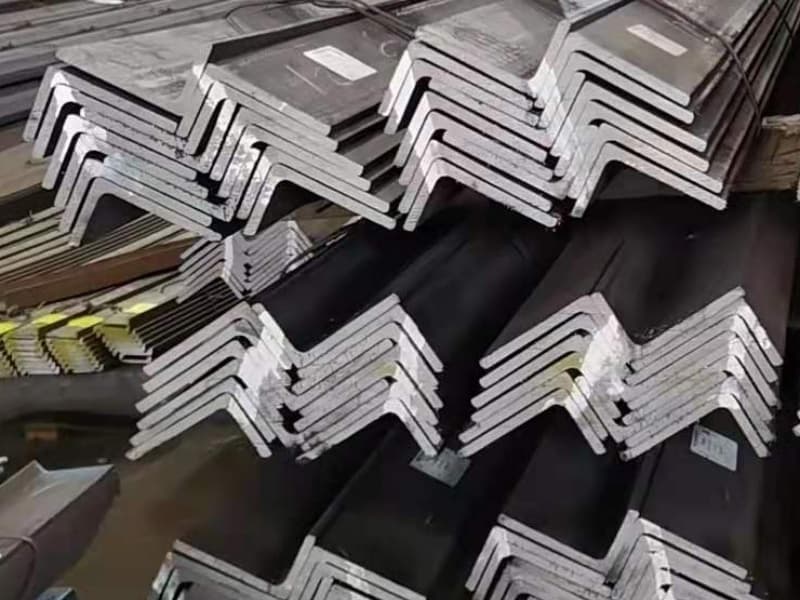
A paper-only sheet and an auditable sheet look similar on page one. They behave very differently when something goes wrong.
| Feature | Paper-only sheet | Auditable sheet |
|---|---|---|
| Header | Title and date | Drawing number, revision, issue status, preparer |
| Rows | Size and quantity | Block, profile, grade string, cut length, positions, kg/m, weight |
| Changes | Overwritten in place | Logged with delta and signature |
| Weight basis | Copied from a summary | Rebuilt from table kg/m |
| Traceability | Added after delivery | Heat reference filled at allocation |
| Handoff | Emailed PDF | One locked file plus a bar count for purchasing |
| Dispute outcome | Re-measure and argue | Ten minutes of arithmetic |
Conclusion
A reliable takeoff sheet is a controlled document, not a spreadsheet. Lock the revision, name every column, run three checks, and the order stops being a guess.