The block is ready, the welders are booked, and the angle steel is still at sea. One late bundle idles a whole bay while the erection date refuses to move.
Plan marine angle steel around a tight assembly schedule by working backwards from the erection date. Fix the date when each block’s full stiffener kit must be on the shop floor, cut and ship to that date, hold one buffer at the material gate, and never release a block without its complete kit.
Most yards I visit plan angle steel as a purchase order line with a delivery date. Then they plan the block as a separate exercise with a start date. The two plans meet in the assembly hall, and that is where the argument happens. I have sat in that meeting more than once, and the yard almost always loses it, because the block start date was set by a planner who assumed the steel would be there.
So let me show you the planning method I use with buyers who run tight block schedules. It is not complicated. It is just uncomfortable, because it forces you to name the date when the steel has to be physically on the floor, not the date it is supposed to leave the mill.
Why Does Marine Angle Steel Decide the Block Assembly Date?
Plating arrives early. Frames, ribs and brackets arrive last. So the profile list, not the plate list, is what sets the day a block can leave the bay.
Marine angle steel decides the block assembly date because stiffeners are fitted after the plating is welded, and a block cannot leave the bay until every frame and bracket is in place. One short section stops a finished block, however complete the rest of the kit is.
Every block flows through the same gates. Plates are blasted and primed, cut, welded into panels on the panel line, then joined with sub-assemblies into a three-dimensional block. Fitting and welding labour peaks at that block assembly stage. After that comes pre-outfitting, then blasting and painting, then transport to the berth.
The panel line sets the rhythm, but the profile list sets the finish
The panel line is highly productive and completely inflexible. It has a fixed throughput, and it only likes flat, repetitive structure. That makes it the pacing item when a yard pushes many flat blocks through at once. Planners watch it closely because it is easy to watch.
The angle steel is harder to watch. It arrives in bundles, it gets cut into hundreds of small parts, and it disappears into sub-assembly and block assembly where nobody counts it until something is missing. But the block cannot be signed off until the last bracket is welded, and the paint hall will not take a block with frames still missing. So the profile list quietly owns the end date of every block.
Kit rate matters more than fill rate
This is the single idea that changes how a buyer should plan. A shipment can be 96 percent complete by tonnage and still stop a block dead, because the missing four percent is one unique section that belongs to one block.
That is why I ask buyers to track a kit rate, not a fill rate. A kit rate counts blocks that can start with 100 percent of their bill of material on the floor. A fill rate counts tonnes landed against tonnes ordered. The first number tells you whether the yard can work tomorrow. The second number tells you whether the invoice matches the packing list. Both matter, but only one of them protects the schedule.
I watched this play out at a yard in [Zora will replace] last year. Four bundles came off the truck, all the right tonnage, all the right grade. The bracket ring for the engine room block called for L150 × 90 × 10. What was inside the bundle was L150 × 90 × 12. Two millimetres of leg thickness, one week of block assembly, and a very quiet meeting with the production manager.
| Block stage | What the angle steel has to be | What a one-week slip actually costs |
|---|---|---|
| Sub-assembly | Cut brackets, web stiffeners, small frames | Sub-assembly bay holds half-built units; block assembly starts late |
| Block assembly | Frames, ribs, deck beams, bracket ring | Bay occupied, fitters and welders idle, crane slot lost |
| Pre-outfitting | Small support angles, hangers, seatings | Outfitting crew works around missing steel, then returns |
| Blast and paint | Nothing, but the block must be complete | Paint booth slot lost; coating intervals cannot be compressed |
| Erection | Nothing, but the block must arrive on time | Dock sequence breaks, and the whole ship moves |
That last row is the one that hurts. A paint booth is booked weeks ahead, and coating cure intervals are not negotiable. When a block misses its paint slot, it does not lose one day. It waits for the next free slot, which is often a week or more.
The steel nobody tracks is the steel that stops the block
Plates get tracked because they are expensive and easy to count. A 12 m plate is a visible object, and the stockyard knows exactly where it sits. Angle steel is different. It arrives as a bundle of small bars, it gets cut into pieces that fit in a hand, and by the time it reaches block assembly it is mixed into a trolley with forty other parts.
So when a block stalls, the first question is always about plates, and the answer is always that the plates are fine. The second question is about profiles, and that is where the silence starts. If your material tracking does not follow angle steel down to the block and the frame, you will keep discovering shortages at the worst possible moment, which is the day the block is supposed to be closed.
How Do You Build a Fabrication Plan Backwards from the Erection Date?
Start at the day the block must be standing on the berth, then subtract each stage. Whatever date is left is the day your steel has to be in the yard.
Build the plan backwards: erection date minus transport, paint, outfitting and block assembly gives the block start date. Subtract sub-assembly and cutting, then subtract receiving and inspection. The remaining date is the date the steel must physically be on your floor, not the date it leaves the mill.
I use a simple planning template for this. The durations below are typical yard assumptions, not measurements from one specific shipyard, so replace them with your own production data before you commit to a date. The structure is what matters.
| Step, counted backwards from erection | Typical duration | Resulting milestone |
|---|---|---|
| Erection on the berth | Day 0 | Block lifted and aligned |
| Transport from hall to dock, alignment | 7 days | Block leaves the fabrication hall |
| Blast and paint, including coat intervals | 5 days | Block enters the paint booth |
| Pre-outfitting inside the block | 6 days | Outfitting complete |
| Block assembly, fit-up and welding | 15 days | Block assembly starts |
| Sub-assembly of frames and brackets | 8 days | Cut parts released to sub-assembly |
| Cutting, including first-piece checks | 7 days | Bars released to the saw |
| Receiving, counting and dimensional check | 5 days | Steel on the yard floor |
Add those up and the steel has to be in your yard about 54 days before erection. Then add the shipping leg. From Qingdao to Dammam the vessel takes roughly 18 to 22 days, and mill production runs another 10 to 15 days. That puts the purchase order roughly 85 to 95 days ahead of the erection date for a Saudi project. Most schedules I am shown allow 60.
The voyage cadence is monthly, not weekly
Here is the detail that catches planners out. Container service to the Gulf is frequent, but a full project volume of angle steel usually moves breakbulk, and breakbulk sailings from Tianjin or Shanghai to Dammam run roughly once or twice a month. Booking windows close 15 to 20 days before sailing.
So a missed booking does not cost you a week. It costs you a month. Any plan that assumes a late bundle can be recovered on the next vessel is really a plan that assumes the block will wait four weeks.
That is why I now push buyers to fix the sailing, not just the production date. Once the vessel is named, the production date becomes real, the inspection date becomes real, and the yard can plan the block around a date that will not drift.
Put the buffer at the material gate, not at the end
Every yard adds some float. The question is where. Most add it at the end, in the form of an erection date everyone knows is soft. That float gets consumed quietly, one small delay at a time, and nobody notices until the dock schedule is already broken.
I prefer to put the float at the material gate. Hold two to three blocks worth of the fast-moving sections in the yard at all times, and let that stock absorb mill delays, voyage delays and inspection findings. Then the block sequence runs without float, because the material risk has already been paid for.
This costs warehouse space and working capital. It also converts a schedule that fails once a quarter into a schedule that holds. For a yard building a series, the trade is almost always worth it.
Label by block, not by size
The cheapest schedule improvement I know costs almost nothing. Ask the mill or the supplier to tag each bundle with the block number it belongs to, not just the size and heat number.
A bundle that says L100 × 100 × 10 tells a storeman what it is. A bundle that says Block B07 tells a fitter where it goes. The second label removes a search, a sorting step and an argument. When I shipped the first block-tagged order to our Dammam distributor, the feedback that came back was about the packaging, not the steel. That surprised me at the time. It should not have. Packaging is the part of the delivery the yard touches first.
If you want the full document set that supports that labelling, our marine angle steel documentation checklist covers the certificates, packing lists and bundle marks that should travel with the steel.
Which Details Break a Tight Plan on the Shop Floor?
A plan built on a calendar ignores geometry. Tolerance stack is what turns a comfortable schedule into a week of grinding and re-cutting.
The details that break a tight fabrication plan are tolerance stack, bar length, marking and traceability. Leg, thickness and straightness tolerances outside EN 10056-2 limits turn a planned 1 mm gap into a 4 mm gap, and every extra millimetre of gap is fitter hours you did not schedule.
The tolerance stack, in numbers you can use
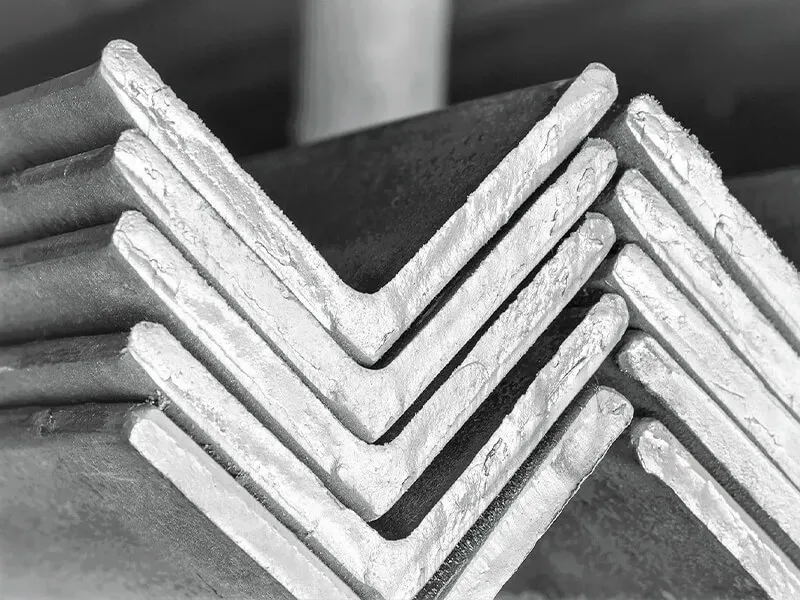
EN 10056-2 governs hot-rolled angle tolerances. Leg length is allowed to run plus or minus 1.5 mm on sections up to 100 mm leg, and about plus or minus 2 mm on larger legs. Thickness is allowed plus or minus 0.5 mm up to 5 mm, roughly plus or minus 0.75 mm between 5 and 10 mm, and up to plus or minus 1.2 mm above 15 mm. Squareness is 90 degrees plus or minus 1 degree. Straightness is the number that matters most for fit-up.
On a 12 m bar, the standard straightness limit of 0.4 percent of length allows 48 mm of bow. A tighter 0.2 percent allows 24 mm. A 0.1 percent specification allows 12 mm. That difference is not cosmetic. A bowed bar pulls the frame out of line, the fitter closes the gap with a jack, and the tack weld locks that stress into the block. When the jack comes off, the frame springs back and the next frame no longer lines up.
I have argued for the tighter straightness on frame-heavy blocks for years. It costs a little more at the mill and saves far more at the fit-up stage, because it removes the jacking step completely on most frames.
Bar length will break a nesting plan built on spare millimetres
Mill lengths are usually supplied to a tolerance of 0 to plus 50 mm. A nest that leaves 30 mm of spare on a 12 m bar is not a nest, it is a hope. That bar can arrive at 11.95 m and the last part will not fit.
Keep at least 100 mm of slack per bar in the cutting plan, and always account for one kerf per cut. If you want the full method, our guide to marine angle steel cutting sequences walks through longest-first nesting and bar release order.
Traceability is a schedule item, not a paperwork item
A class surveyor can ask to see the heat number on a frame that is already welded into a block. If the remnant was cut without transferring the original marks, that conversation gets expensive. The practical rule is that leftover pieces keep their original mill marks, and every cut part keeps a tag that points back to a heat number and a mill certificate.
This is also why the receiving inspection has to happen at the material gate and not at the saw. Checking dimensions, marks and certificates when the truck arrives costs a few hours. Discovering a problem after the bars are cut costs the block.
| Parameter | EN 10056-2 limit | Effect on a tight schedule | What I would specify |
|---|---|---|---|
| Leg length | ±1.5 mm up to 100 mm leg, ±2 mm above | Frame spacing drift, uneven gaps at brackets | Standard limit, checked at receiving |
| Thickness, 5 to 10 mm | About -0.5 / +0.8 mm | Weight and weld prep variation, root gap wander | Standard limit, with MTC check |
| Straightness | 0.4% of length for legs ≤150 mm | Bow pulls frames out of line, jacking and spring-back | 0.2% for frame-heavy blocks |
| Straightness, legs over 200 mm | 0.2% of length | Same, but with heavier sections and more force | 0.1% where frames are long |
| Squareness | 90° ±1° | Toe gap at fillet welds, extra grinding | Standard limit, spot-check at receiving |
| Length | 0 to +50 mm | Nesting plan fails on the last part | 100 mm slack per bar in the nest |
None of these limits is exotic. The problem is that yards plan as if every bar lands on nominal, and then absorb the difference with fitter hours that were never in the budget.
Which Planning Approach Holds When the Schedule Compresses?
Three approaches are common. Only one survives a compressed schedule, and it is the one that treats angle steel as a kit rather than a tonnage.
The approach that holds under compression is block-kitted ordering with a small safety stock of fast-moving sections. Ordering by tonnage optimises freight and loses the block. Ordering every block separately optimises the block and multiplies freight. The hybrid keeps both.
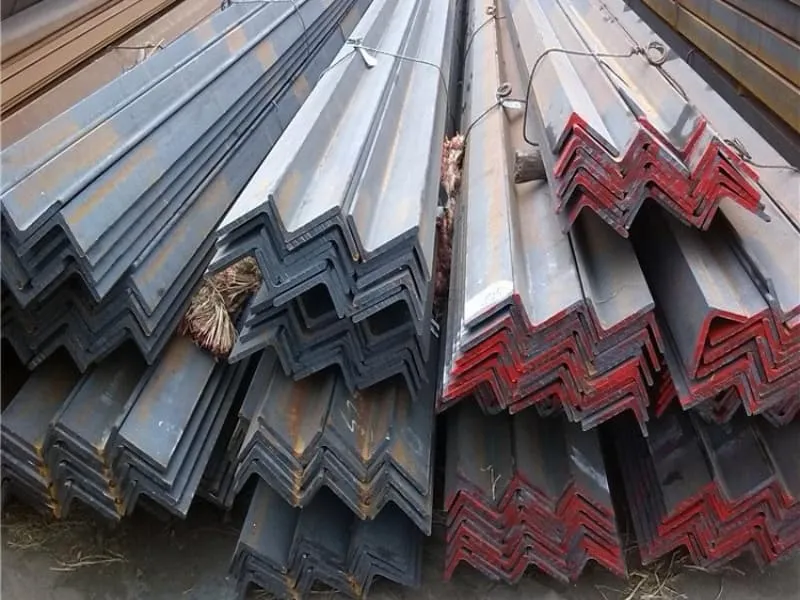
The tonnage approach treats angle steel like plate. You estimate total tonnes, round up for waste, order one large lot, and let the yard sort it out. Freight per tonne is excellent. The problem is that the lot is sized for the whole ship, so the sections needed by the first block arrive mixed with sections needed by the eighth. The yard then spends weeks sorting, and the first block waits on a section that is technically already on site.
The per-block approach fixes that, but it multiplies shipments and freight, and it leaves no material for the small unplanned jobs that always appear.
The hybrid is what I recommend. Split the list into two groups. Fast-moving sections that appear in many blocks go into a standing stock of two to three blocks worth, replenished on a rolling basis. Project-specific sections, the odd unequal-leg sizes and the thick brackets, get ordered as block kits against a fixed kit date. Then the plan has one buffer and one hard date per block.
What the split looks like on a real list
Take a typical handysize programme, roughly [Zora will replace] tonnes of angle steel across twelve blocks. Six or seven sections do most of the work: the main frame angle, the deck beam angle, and two or three bracket sizes. Those belong in standing stock. The rest, maybe eight or ten section sizes that appear in one block each, belong in kits.
Doing the split takes an afternoon with the block bills of material open. Doing it before the order goes out saves the weeks that the yard would otherwise spend sorting a mixed pile. If the block list is still moving, keep the kit quantities loose and let the stock absorb the uncertainty, because stock can be used anywhere and a kit cannot.
Then check the kit date against the vessel, not against the mill. The mill will always quote production days. The vessel is the thing that decides whether those production days are early enough.
| Approach | Kit certainty | Freight cost | Yard sorting | Best suited to |
|---|---|---|---|---|
| Single tonnage order for the whole ship | Low in the first blocks | Lowest | Heavy, weeks of sorting | Yards with large storage and loose schedules |
| Per-block kits only, no stock | High | Highest | Minimal | One-off projects with a fixed block sequence |
| Hybrid: stock plus block kits | High | Medium | Low | Series building and repeat programmes |
| Order by size, cut from general stock | Medium | Low | Medium | Yards with a strong internal cutting plan |
I have never seen a yard regret the hybrid. I have seen several regret the single big order, usually in the week the first block is supposed to start.
Conclusion
Plan angle steel from the block backwards, kit it by block, and hold the buffer at the material gate. The erection date then stops being a hope.