You ordered the right marine angle steel. Your saw team cuts it in a random order. Parts pile up, heat twists the profiles, and the assembly line stands still waiting. A planned cutting sequence fixes this.
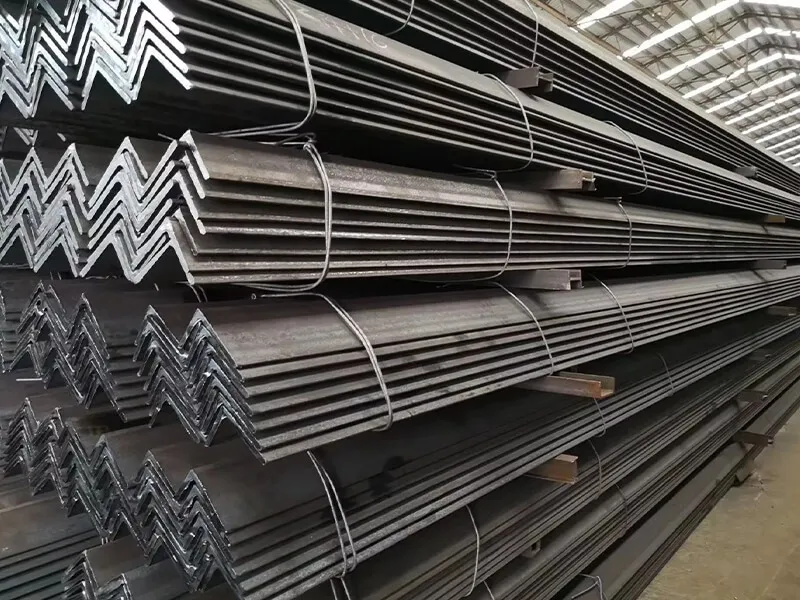
Plan marine angle steel cutting sequences by sorting the cut list by size and assembly stage, nesting longest-first with kerf allowance, cutting the stiffest parts first, supporting both sides of every cut so residual stress releases safely, and checking the first piece from each bar before committing the whole batch.
Most buyers I talk to think cutting is a workshop problem, not a procurement problem. I disagree. When I visited a fabrication shop in Vietnam last year, I watched two teams cut the same grade of angle steel on the same day. One team worked from a printed nesting plan taped to the saw bench. The other worked from a verbal queue. The first team finished their batch four hours earlier, with less scrap and no re-cut. The difference was not the steel. It was the sequence. In this article I will walk you through how we help our clients plan cutting sequences that hold up on the shop floor — from sorting the cut list, to controlling heat and residual stress, to locking the sequence to the assembly schedule.
Which Order Should You Cut Marine Angle Steel Bars In?
The saw is idle, the bars are stacked, and the foreman points at whatever bar is closest. So cutting starts late and ends in confusion, and nobody can trace which part came from which heat number. A fixed cutting order removes all three problems at once.
Cut marine angle steel bars in this order: sort the cut list by grade and section size first, then nest each size group longest-part-first into stock bars with one kerf per cut, then release bars to the saw in the same order the assembly line will consume the parts. The cut list decides the sequence, not the stack.
Sorting sounds like paperwork. It is actually the step that decides whether your sequence works at all. In Chinese shipyard practice this discipline is written down explicitly — GB/T 37535-2019 advises yards to complete the nesting calculation before ordering and to select steel specifications from the nesting results rather than from rough estimates. The same logic applies one level down, at the saw: the sequence should be built from the cut list, not from the order bars happen to sit in the yard.
Sort Before You Saw
Group the cut list by grade, then by section size, then by length. A mixed list is the enemy of a good sequence. I learned this the hard way early in my export work: a buyer sent me one merged list where L100×100×10 and L150×90×9 parts were tangled together. His workshop spent a week just re-sorting bars on the ground before a single cut was made. Nothing was wrong with the steel. The order was just organized for the seller instead of the saw. Now I ask every client for the split before I quote, because the split is what makes a cutting sequence possible.
Nest Inside Each Group
Within each size group, apply first-fit-decreasing: sort the required part lengths from longest to shortest, place each into the first stock bar that still has room for the part plus one saw kerf, and only open a new bar when nothing fits. This is not the mathematically perfect answer, but it is what a good foreman does with a pencil, and it routinely brings waste down to the 3 to 5 percent range against 10 to 15 percent for unplanned cutting. Keep at least 100 mm of slack per bar in the plan — EN 10056-1 gives mill lengths a tolerance of 0/+50 mm, so a bar that arrives at 11.95 m will break a nest planned with only 30 mm to spare.
Release Bars in Assembly Order
Here is the step most yards skip. After nesting, re-order the bar release queue so the parts come off the saw in roughly the order the assembly line needs them. If the transverse frames are welded before the longitudinal stiffeners, the bars carrying frame parts go to the saw first. This single habit cuts the time parts spend waiting in trolleys, and it makes heat-number tracing easy, because each released bar carries its own tag through the whole sequence.
Plan the Restock Inside the Sequence
A cutting sequence also has to answer a simple question: what happens when the last bar of a size group runs out mid-batch? If the answer is “stop and wait for the next delivery”, the sequence collapses. Check stock coverage before the first cut. If a group needs five 12 m bars and only four sit in the rack, either split the batch so the fifth bar’s parts move to a later release, or confirm the replacement bar’s arrival date before the saw starts. Bars from different mill heats can also carry slightly different straightness and surface condition, so a mid-batch change of heat should be planned, not discovered. I ask clients to send us their cutting calendar when they order. Then we can match the delivery schedule to the release schedule, so a new batch of marine angle steel lands at the gate a day or two before the rack runs empty. Steel sitting in your yard for two extra months is money parked on the ground. Steel arriving two days late stops your saw. Both are planning failures, and both are fixable with one email.
How Do Heat, Residual Stress, and Saw Choice Change the Cutting Order?
You have a nesting plan, so the lengths are right. But halfway through a bar, the offcut pinches the blade, or the part comes off the saw with a twist, and now your sequence is broken by rework. The order of cuts and the cutting method both feed into this.
Sequence cuts so the bar stays supported on both sides and residual stress releases gradually: cut the stiffest, longest parts first, leave the offcut attached until the final cut, and prefer low-heat saw cutting over thermal cutting when the cut face is a welding fit-up surface. A stable bar keeps the whole sequence honest.
Let the Residual Stress Out Safely
Every rolled bar carries internal stress from the mill. A cut releases it. If the offcut is unsupported when the cut completes, it can drop, pinch the blade, or tear the final edge. Support the bar on both sides of every cut, and account for the center of gravity on long lengths. I stood next to a bandsaw in [Zora will replace] where an unsupported 12 m bar sagged at the last cut and the piece came out 4 mm out of square. The whole batch had to be re-measured. One roller stand would have prevented that afternoon.
Watch the Heat, Cut in the Right Order
Thermal cutting puts heat into a small area, and heat builds up along a long bar. On asymmetrical profiles like unequal-leg angle, one side of the section expands more than the other, and the bar can bow as you cut. Sequence thermal cuts to spread the heat: if the machine allows it, alternate cuts between bars rather than burning a full bar end to end, and let thick sections cool between cuts. On automated profile lines — the modern ones feed bars through a buffer, mill and blast the edges, mark and robot-cut, then sort the parts automatically — the machine handles this sequencing for you. On manual saws, the operator is the sequencer, so the plan has to say explicitly which cuts to spread out.
Pick the Method That Fits the Sequence
The cutting method changes the kerf you must budget into every nest, and it changes the heat you must spread through the sequence. Measure the kerf on your own saw with a test cut instead of trusting the catalogue, because blade wear moves the number over time.
| Cutting method | Typical kerf per cut | Heat input | What it means for the sequence |
|---|---|---|---|
| Bandsaw (bimetal) | 1.1–1.6 mm | Very low | Best for fit-up faces; sequence can run tight back-to-back cuts |
| Cold saw | 2–2.5 mm | Low | Clean square cuts; fine for mid-size batches |
| Abrasive cut-off | 2.5–3 mm | Medium to high | Fast but hot; spread cuts and expect edge cleanup |
| Plasma | 1.5–4 mm | High | Watch distortion on thin and unequal legs; alternate between bars |
A 46-piece line at 3 mm per cut loses around 140 mm of steel to dust — enough to push one extra bar into the order if kerf was ignored. And remember that a thermally cut edge carries oxide and dross that a welder must grind off before fit-up, while a sawn face is often weld-ready. When the cut face is a critical fit-up surface, the saw is usually the right answer even if it is slower.
Sequence Coping and Notch Cuts with Care
Most angle parts need more than a square end cut. Brackets get coped, stiffener ends get sniped, and frame parts get notched where they land on another member. These secondary cuts change the sequence too. Do them in a fixed order: square length cut first, then cope or notch, then bevel, then hole punching or drilling if the part needs it. When each operation happens in the same order on every part, operators build rhythm, and fixtures stay set up for the whole batch instead of being changed part by part. One fabricator we work with in [Zora will replace] cut punching before coping for years, and every punched hole drifted as the cope released stress near it. Swapping the two steps fixed the drift without buying any new machine. The lesson I took from that visit: the sequence is not just which bar gets cut when. It is also which operation touches the part first.
How Do You Sync the Cutting Sequence with the Assembly Schedule?
Your saw team is producing beautiful parts. But the assembly crew needs brackets today and stiffener bars next week, and your sequence delivers them in the opposite order. So parts wait, trolleys overflow, and the sequence you planned becomes a sorting problem again.
Sync the cutting sequence with the assembly schedule by breaking the cut list into the same work packages the assembly line uses, releasing one package at a time to the saw, confirming the first piece of each package against the drawing, and staging cut parts by package so nothing gets re-sorted on the floor.
Cut in Work Packages, Not in Bar Order
The assembly line does not consume steel one bar at a time. It consumes one block, one panel, or one frame unit at a time. So the cutting sequence should follow those units. Take the material list for one assembly unit, nest it, cut it as one release, and deliver it as one labeled batch. When we supplied a project distributor in Saudi Arabia, their fabricator told us that switching from bar-order cutting to unit-order cutting removed most of the daily floor sorting — the parts now arrive where the welders need them, in the order the welders need them.
Verify the First Piece from Each Bar
Before the batch runs, cut one part and check it: overall length, squareness, and bevel angle where the drawing calls one. This short pause is far cheaper than sorting a full batch of nonconforming parts later. On thermally cut parts, also inspect the edge — dross, gouging at starts and stops, and burrs all become weld-prep work. I tell every client the same thing: the first piece is your proof that the sequence, the kerf allowance, and the setup all agree. If it passes, commit the batch. If it fails, fix the plan before bar two, not after bar forty.
Stage and Tag the Output
Each cut part should leave the saw bench with a tag: heat number, section size, part mark, and the assembly unit it belongs to. Heat number transfer matters for classification records, and the part mark prevents the kind of mix-up I saw early in my career — a close-size angle meant for longitudinal stiffeners installed as transverse frames, and two weeks of rework to undo it. Stage the tagged parts in trolleys or racks by assembly unit, not by size. The next handler should never need to think.
Close the Loop with a Short Daily Review
A sequence plan is a hypothesis. The shop floor proves or breaks it every day. I encourage clients to hold a five-minute review at the end of each shift: which releases finished on time, which bar broke its nest, which first piece failed. Three numbers on a whiteboard are enough — parts cut, parts rejected, and releases delivered to the assembly line on schedule. After a week, the pattern is obvious. Maybe the nesting numbers are right but the saw crew runs out of roller stands. Maybe plasma parts always need extra grinding, so the bevel allowance needs adjusting. When we ship marine angle steel to a new client, I ask for that first-week review, because it tells us whether the supplied bar lengths actually fit their nesting plan. If not, we adjust the next order to different mill lengths, and the waste never reaches the shop floor at all. A cutting sequence that is reviewed becomes better every week. One that is not reviewed stays exactly as good as the day it was written.
Now compare the two ways of running the saw, side by side:
| Aspect | Unplanned cutting sequence | Planned cutting sequence |
|---|---|---|
| Cut list basis | Verbal queue, nearest bar first | Sorted, nested, kerf-budgeted plan |
| Material waste | 10–15% typical | 3–5% typical |
| Part flow to assembly | Random order, heavy re-sorting | Released in assembly-unit order |
| Residual stress control | Offcuts unsupported, blade pinch risk | Both sides supported, stress releases gradually |
| Heat management | Bar cut end-to-end, distortion builds up | Cuts spread across bars, sections cool |
| Quality check | Batch inspected after completion | First piece verified before batch commit |
| Traceability | Heat numbers hard to track | Each bar and part tagged through the sequence |
| Typical outcome | Idle welders, rework, overflow trolleys | Steady part flow, clean fit-up, fewer surprises |
Conclusion
Plan the cutting sequence from the cut list, protect the bar from stress and heat, and release parts in assembly order — the saw, the welders, and the budget all stay aligned.