A stockout on a fast-moving angle size stops a hull line cold, and panic spot-buying then costs you price, quality control, and weeks. I will show you the classification, safety stock math, and reorder discipline that keep the common sizes on the floor.
Prevent stockouts of frequently used marine angle steel sizes by classifying every leg-thickness-length-grade combination into A/B/C classes, setting a calculated safety stock per class (2–3 weeks of cover for A items), placing replenishment orders at a computed reorder point, and reviewing A-class positions weekly with your mill or stockist.
Shipyard buyers rarely lose a project because the mill could not roll the steel. They lose time because the size they needed this week was the one somebody forgot to reorder three weeks earlier. I have walked enough yards between Quảng Ninh and Dammam to know the pattern, and the fix is boring, numerical, and completely within your control. Let me break it down.
What Actually Causes Stockouts in Frequently Used Marine Angle Steel Sizes?
Your racks hold twelve fast movers today, and next month one of them is empty while three slow movers gather dust. That imbalance is not bad luck — it is a forecasting and replenishment system that never learned your own consumption rhythm.
Stockouts in frequently used marine angle sizes come from five causes: unclassified stock treated as one pool, demand pulses from block erection schedules, a reorder point based on gut feel instead of consumption data, supplier lead times treated as fixed when they are not, and remnants that disappear from the ledger the moment a bar is cut.
The Demand Is Pulsed, Not Smooth
Shipbuilding does not consume angle steel the way a factory consumes bolts. Demand arrives in pulses: the design office freezes a structure, procurement releases one large order, the blocks eat through your stock in a fortnight, then nothing for a month until the next structure starts. I watched a Vietnamese yard burn through their entire position of L100×100×10 — 15.12 kg per metre, about 181 kg on a 12 m bar — in nine working days when the double-bottom line accelerated. Their replenishment plan assumed flat weekly consumption, so the reorder trigger fired weeks too late.
This is why a plain moving average lies to you. Steel distributors using forecasting methods track this properly: a 3–6 month rolling average works for stable products, exponential smoothing with an alpha of 0.2–0.4 weights recent months more heavily, and qualitative inputs from the yard’s block schedule matter more than any formula. When the yard tells you a hull section launches in March, believe the schedule over the spreadsheet.
The Unclassified Rack Problem
Treat every angle size identically and you guarantee stockouts on the movers and dead stock on the rest. A working classification crosses product family, grade, and size against annual usage value. The distributors’ data is consistent: roughly the top 20% of SKUs carry about 80% of the value, the next 30% carry about 15%, and the bottom half carry about 5%. For marine angle, the A class is predictable — L75×75×6 through L150×150×12 in grade A or AH36, the frame and bracket sizes every hull uses. B class covers unequal legs like L125×80×8. C class covers the oddballs you roll once a year.
Here is my port-side observation after years of shipping angle steel: the sizes that cause stockouts are almost never exotic. It is the humble L75×75×6 — 6.78 kg per metre, four in every five hulls — that goes missing, because everybody assumes somebody else is watching it.
The Certificate Gap Turns a Shortage into a Stoppage
Grade mixing deserves its own warning. When the fast mover that runs out is grade A, a substitute from another stockist is a phone call away — standard structural grades are interchangeable between reliable suppliers. When the fast mover is AH36 endorsed by a specific society, the shortage hardens into a stoppage, because the yard’s approved welding procedure, the mill test certificate, and the classification survey all point at one grade from one traceable heat source. I have seen a bracket fabrication cell sit idle for four days over exactly this: plenty of angle steel on the racks, none of it the certified grade. The practical rule I give buyers: identify which of your fast movers are certificate-locked, and either widen their safety stock or pre-position a buffer with a supplier who holds society-certified stock — that is precisely why we keep CCS, ABS, DNV, LR, BV, and KR certified positions in our Liaocheng warehouse rather than ordering against each enquiry.
The ledger also lies about what is really on hand. Physical stock and system stock drift apart through unlogged remnants, bundles opened for samples, and pieces moved between racks without a transaction. By the time a monthly count exposes the gap, the reorder trigger has been silently broken for weeks. Accuracy needs continuous cycle counting rather than one annual reconciliation, and every movement — issue, transfer, remnant return — needs a transaction the same hour it happens.
| Stockout cause | Early warning signal | Corrective action |
|---|---|---|
| Unclassified stock | All sizes reviewed at the same monthly frequency | Run ABC × grade-size matrix; review A weekly |
| Pulsed demand | Reorder triggers fire late after big block releases | Feed the yard’s block schedule into the forecast |
| Gut-feel reorder point | Stockouts despite “enough” average stock | Compute reorder point from lead time demand plus safety stock |
| Variable lead time | Supplier quotes keep slipping 2–3 weeks | Track actual lead time deviation; widen σLT in the math |
| Vanishing remnants | Ledger shows bars that physically no longer exist | Tag and re-enter remnants over ~2 m as tracked stock |
How Much Safety Stock Should Each Marine Angle Size Carry?
Carry too little and one delayed vessel strands your frame line. Carry too much and your money sits in rusty iron while holding costs of roughly 10–15% per year quietly eat the margin you negotiated so hard for.
Set safety stock per angle SKU with the formula Z × √(lead time × σD² + demand² × σLT²), using Z = 1.65 for a 95% service level, then adjust: add 20–30% cover for long-lead imported grades, trim 10–15% when prices swing more than 5% a month, and hold A-class fast movers at 2–3 weeks of cover reviewed weekly.
Do the Math Once, Per Size
The formula looks intimidating, so let me walk a real number set. Take L100×100×10 in grade A, consumption of 40 bars per month, demand standard deviation σD of 10 bars, and an actual measured lead time of 1.4 months with a σLT of 0.25 months. Safety stock equals 1.65 × √(1.4 × 10² + 40² × 0.25²) = 1.65 × √(140 + 100) ≈ 1.65 × 15.5 ≈ 26 bars. That is your buffer — roughly 4.7 tonnes of this one size. Skip the calculation and people either carry a superstitious “three bundles of everything” or carry nothing and pray.
Two steel-specific adjustments matter. Standard structural grades substitute easily between suppliers, so standard safety stock holds. But a specification like AH36 with a specific classification society endorsement — ABS, DNV, LR, BV, KR, or CCS — is harder to replace at short notice because the mill test certificate must match the approved grade. If your project certificates are locked to one society, widen the safety stock for those grades or pre-position stock at a port warehouse. And when a substitute arrives that is theoretically equivalent, remember the certificate problem: a yard cannot weld AH36-certified structure from undocumented bars, no matter how good the steel looks.
Classification Sets the Review Rhythm
The policy table below is the one I hand to buyers setting up a stockyard from scratch. It borrows the standard distributor practice of matching review frequency and cover weeks to class.
| Class | Share of SKUs / value | Review cadence | Safety stock target | Typical marine angle examples |
|---|---|---|---|---|
| A | ~20% SKUs / ~80% value | Weekly | 2–3 weeks of demand | L75×75×6, L100×100×10, L150×150×12, grade A / AH36 |
| B | ~30% SKUs / ~15% value | Every two weeks | 3–4 weeks of demand | L125×80×8, L90×56×7, L100×63×8 unequal legs |
| C | ~50% SKUs / ~5% value | Monthly | 4–6 weeks or make-to-order | Rare leg-thickness combinations, odd lengths |
Measure the System With Four Numbers
Safety stock is only as good as the metrics watching it. I track four numbers for every angle steel customer who runs their own yard stock. Inventory turnover — cost of goods sold divided by average inventory value — should land between 6 and 12 turns per year for common marine grades, with specialty combinations running 4 to 6. Below 4 turns means dead weight; above 15 means you are flirting with stockouts and rush freight. Stockout rate — unfilled demand lines divided by total demand lines — should stay under 2% for A-class sizes. Inventory accuracy needs to hold above 98%, because every phantom bar on the ledger is a stockout you have already bought. And holding cost, combining warehousing, insurance, capital, and obsolescence, runs about 10–15% of inventory value per year — which is exactly why the buffer belongs only on sizes the math justifies, spread evenly across the rack.
One caveat from experience: the C class is where carcass stock hides. Set an aging alarm — anything with no movement for 180 days gets flagged — and force a decision: cut it into remnant kits, offer it to repair yards, or discount it. Dead C-class stock is how yards pay for their A-class service level without noticing.
When Should You Place the Replenishment Order?
The safety stock tells you how deep the buffer runs. The reorder point tells you when to pull the trigger — and getting this date wrong by two weeks undoes all the clever math above.
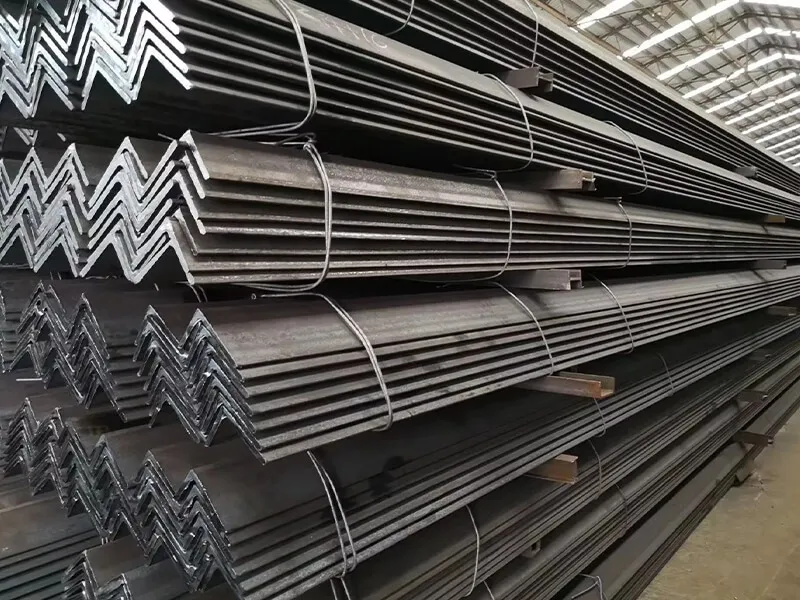
Place the replenishment order when on-hand plus on-order stock for an angle size falls to the reorder point: expected demand over the real measured lead time plus the calculated safety stock. Track the supplier’s actual lead time every delivery, source critical grades from two or three mills, and lock recurring volumes in framework agreements instead of buying in a panic.
Reorder Point in Practice
Continue the L100×100×10 example. Demand of 40 bars per month over a 1.4-month lead time means 56 bars will be consumed before the next delivery arrives. Add the 26-bar safety stock and your reorder point is 82 bars — about 14.9 tonnes. The moment on-hand plus in-transit stock touches 82, the order goes out, no debate. Lead time is where buyers get burned: a mill-backed stockist can ship a regular angle size in days — my own customers in the Gulf get regular sizes in about a week and bulb flat in about a fortnight — but a first-time import order to the Middle East realistically runs 8–12 weeks door-to-door, and breakbulk sailings to Dammam run once or twice a month. If you miss the booking, you do not lose a week; you lose a month. Measure the real lead time per supplier per route, and let the deviation, not the brochure number, feed the formula.
Quality discipline matters inside replenishment too. Every incoming bundle should be checked within hours of arrival — dimensions against the order, mill test certificate against the heat number, surface condition against class expectations — and non-conforming bundles isolated immediately, because a bundle that fails inspection on arrival is functionally a stockout you have already paid for.
Panic Buying Versus Planned Replenishment
This is the comparison I wish every buyer ran before their first stockout. The two approaches diverge on every line, and the table is worth pinning above the purchasing desk.
| Factor | Panic spot-buy after stockout | Planned replenishment at reorder point |
|---|---|---|
| Price position | Premium for urgency; sellers know you are cornered | Framework agreement or index-linked price |
| Lead time | Compressed, unreliable, expediting fees | Measured lead time with known buffer |
| Certificate risk | Whatever grade is available, MTC mismatch risk | Planned grade and society match per PO |
| Handling | Direct mill-to-yard rush shipping, less packing care | Proper bundling, marking, container or breakbulk stowage |
| Impact on yard | Frame line idle, welders reassigned, schedule slip | Steady feed matching the block schedule |
Dual sourcing is the quiet insurance behind that table: keep working relationships with two or three mills for every critical grade, and split your geographic base between domestic and import supply. When one route wobbles, the second fills the gap without a scramble. My own workflow with repeat buyers — Gulf Metal Solutions among them — is exactly this: consumption data in, standing replenishment positions out, and their yards have not idled on missing angle steel since we set the system up. Their feedback on stable quality and packaging holds because the orders are planned, not desperate.
Two final disciplines keep the system honest. First, cycle counting: hold inventory accuracy above 98% by counting continuously rather than annually, because a reorder point computed on a phantom quantity is a stockout with extra steps. Second, remnant control: every cut remainder longer than about 2 m gets re-entered into stock with its size and heat number on a tag, so the ledger and the racks tell the same story. Buyers who skip these two steps blame the mill for stockouts the mill never caused.
Storage Conditions Protect the Buffer You Paid For
A safety stock you cannot ship is not safety stock. Buffers sit longer than flow stock, so they need protection: steel starts oxidising the moment humidity climbs, so keep stored bundles off the ground on timber or steel dunnage raised at least 150 mm, under a roof that does not leak, with relative humidity below 60% where the budget allows. Rotate first in, first out physically — the oldest bundle ships first regardless of which rack is closest to the crane — and re-inspect anything that has sat longer than 90 days for surface condition before it enters a weldment. A corroded A-class bundle converts your best-planned buffer into a claim, and the yard will remember the claim longer than the delivery. When we pack for Gulf customers we follow the same logic on the outbound side: sound bundling, clean marking, and stowage that keeps seawater out, because a buffer that survives the voyage is the last kilometre of the stockout-prevention chain.
If you are building this system against a live project and want a supplier who holds fast-moving angle sizes in stock and ships on measured, not hoped-for, lead times, our marine angle steel inventory and bulb flat steel reference pages are the fastest starting point — or write to me directly and I will send current stock positions.
Conclusion
Classify your angle sizes, calculate safety stock honestly, reorder on measured lead times, and review the fast movers weekly. Stockouts are a system failure, and systems you can fix.